Summary: Safe plate cleaning is a compatibility and process-control decision. Start by identifying carbon steel, stainless steel, cast iron, coating, and contamination; use the least aggressive method that meets the acceptance criteria; and dry immediately. For cookware, USDA guidance favors removing residue, rinsing, and thorough drying, while industrial work instructions should define a visible-clean endpoint, corrosion protection, and a record of chemicals and dwell time. Test a small area first, never mix cleaners, and stop if the surface, coating, or food-contact status is uncertain.
Iron plate cleaning starts with identifying the surface and the risk
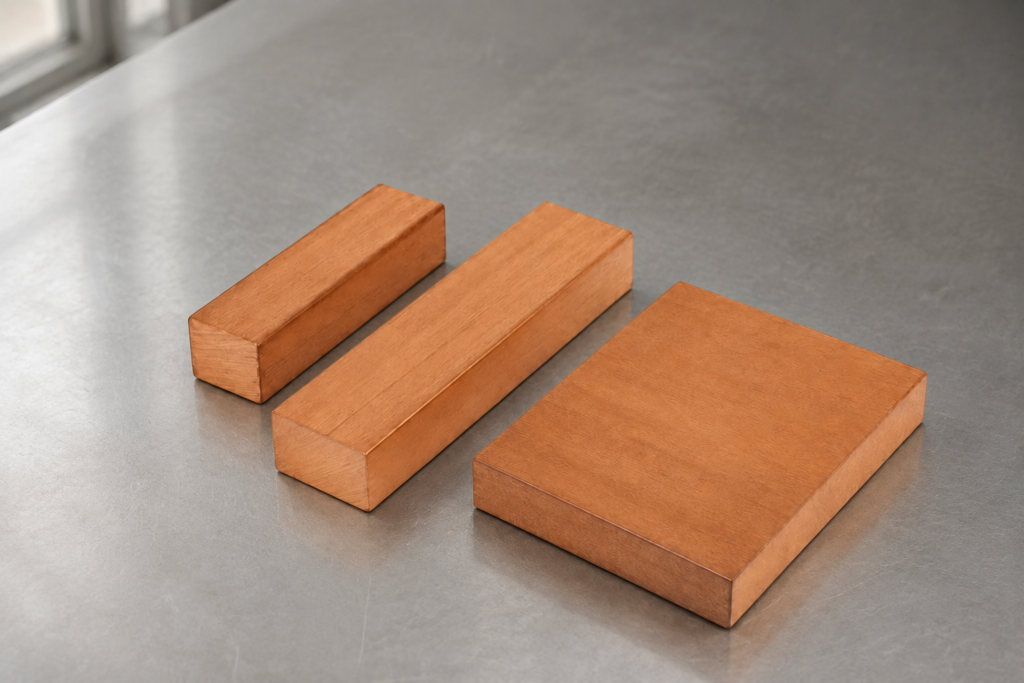
An Iron plate or steel plate may be a structural blank, a busbar support, a machine guard, a tooling plate, or cookware. The same brown mark can be loose soil, mill scale, flash rust, embedded iron, or a coating defect. Cleaning therefore has two goals: remove the contaminant and preserve the surface properties that matter—flatness, roughness, conductivity, weldability, coating adhesion, or food safety. ASTM methods can characterize corrosion or surface preparation, but a test method is not a blanket product certification.
Record the base material, finish, thickness, prior coating, and intended use before choosing a tool or chemical. A magnet can help separate carbon steel from non-ferromagnetic alloys, but it cannot confirm grade; use the mill certificate, drawing, or a positive material-identification process when grade affects the specification. Inspect under good light and photograph the starting condition.
- Carbon steel or bare iron: remove dry dust, then use a neutral detergent and soft nylon brush. A light oil film may be appropriate after drying if the part is not entering a coating or welding operation.
- Cast iron: avoid long soaking. Water trapped in pores and corners accelerates flash rust; heat-dry or towel-dry promptly.
- Painted, plated, or powder-coated plate: start with a compatible neutral cleaner. Abrasives and solvents can expose the substrate or change gloss.
- Food-contact cookware: keep the process simple and repeatable. Do not use industrial rust converters, unknown degreasers, or residues that are not approved for the intended food-contact application.
The first control point is a small-area test, typically on an edge or hidden face. Check color, gloss, roughness, coating adhesion, and whether a white or oily residue remains after rinsing. For production parts, define an acceptance sample and a maximum dwell time rather than relying on the operator’s visual judgment alone.
Cleaning a cast iron grill plate requires a food-contact process
For a cast iron grill plate, allow the surface to cool, scrape loose food with a non-damaging scraper, and brush with hot water and a modest amount of mild detergent when the cookware maker permits it. Rinse until no foam remains, dry immediately, and apply a very thin film of cooking oil before storage. The oil is a seasoning-maintenance step, not a substitute for removing burnt residue.
Do not put a hot plate under cold water: thermal shock can distort a thin section or worsen an existing crack. Avoid steel wool when it sheds fragments, and avoid dishwasher cycles unless the manufacturer explicitly allows them. If the surface is enamelled, treat it as a coated surface; use the coating maker’s limits rather than bare-cast-iron habits.
For industrial plates used near food equipment, separate the cleaning instruction from the cookware instruction. Food-contact suitability depends on the complete material and process, including lubricants, coatings, rinse water, and transfer controls. A plate that looks clean can still carry an unacceptable chemical residue.
How to remove rust from cast iron without over-polishing the surface
Light orange flash rust can often be removed with a nylon abrasive pad, a short application of a manufacturer-approved mild acid, or a chelating product followed by thorough rinsing. The correct choice depends on the grade, geometry, and next operation. Never combine acids, hypochlorites, or alkaline cleaners; incompatible mixtures can release heat or hazardous gas.
When operators need to remove rust from cast iron, use a staged method: (1) brush away loose scale, (2) apply the selected product only for the stated dwell time, (3) rinse with controlled water quality, (4) dry with warm air or a clean lint-free cloth, and (5) protect or season the surface. We recommend measuring pH of the final rinse when a chemical process is used and recording the lot, concentration, temperature, and dwell time. If pits remain, do not grind until the drawing or quality plan confirms the permitted material removal.
For industrial steel plate, rust removal may be part of surface preparation before painting or bonding. ISO 8501-1 visual grades and the coating manufacturer’s preparation requirement can define the endpoint; they do not authorize a particular chemical. A coating inspector may also specify a surface-profile measurement, soluble-salt check, or dust test before application. If the plate will be welded, confirm that the cleaned surface is free of oil, chlorides, and residues that could cause porosity or fumes.
Industrial Iron plate work instructions should control tools, chemicals, and release
A robust instruction names the responsible role, ventilation and personal-protective-equipment requirements, spill response, rinse method, drying step, and release criteria. OSHA’s hazard-communication framework expects workers to have access to chemical hazard information and training; the supplier’s safety data sheet should be available at the point of use. EPA requirements may apply to wastewater, hazardous residues, or disposal depending on the product and jurisdiction.
Use dedicated brushes and containers where cross-contamination matters. A brush used on oily machine parts should not be moved to cookware. For repeat jobs, verify concentration with a simple test or measured mix, use a timer, and retain a batch record. If the process is outsourced, put the acceptance criteria, prohibited chemicals, packaging, and corrosion-protection period on the purchase order.
| Approach | Best fit | Strength | Main risk | TCO implication |
|---|---|---|---|---|
| Dry wipe and soft brush | Loose dust, light soil | Minimal water and chemical exposure | Will not remove bonded rust | Lowest setup cost; may require a second pass |
| Neutral detergent and rinse | Oil, food residue, handling soil | Broad compatibility | Flash rust if drying is delayed | Low consumable cost; drying labor matters |
| Non-woven abrasive pad | Light oxidation on bare metal | Fast, controllable spot work | Can alter appearance or profile | Good for small lots; inspect pad shedding |
| Approved chemical rust remover | Stubborn oxide or pits | Reaches irregular geometry | Residue, attack, fumes, waste | Higher control and disposal cost |
| Mechanical blasting or power tool | Large industrial areas before coating | High throughput | Profile change, dust, embedded media | Equipment and containment can dominate TCO |
| Dimension | Question to answer | Evidence to retain |
|---|---|---|
| Material | Is it carbon steel, cast iron, stainless, or coated? | Drawing, certificate, or verified identification |
| Contamination | Is the mark soil, oxide, salt, paint, or embedded metal? | Photo and simple test result |
| Next operation | Will it be cooked on, welded, painted, bonded, or stored? | Process traveler and acceptance criteria |
| Environment | Can the area control fumes, wastewater, and drying? | SDS review, ventilation check, disposal route |
| Release | What visible and measurable condition permits use? | Inspector sign-off, rinse/pH or profile record where applicable |
Standards and compliance should match the use case
Use USDA public guidance for general food-safety handling principles, OSHA 29 CFR 1910.1200 for hazard communication in the workplace, and EPA rules relevant to chemical residues and wastewater in the destination jurisdiction. ASTM standards can provide repeatable test methods for corrosion, coatings, or surface characterization; verify the current edition and purchase scope before writing a contract. ISO 8501-1 is commonly used for visual cleanliness of steel before coating, while the coating system supplier may add profile, dust, or salt limits.
Commercially, unsupported claims such as “food-safe,” “corrosion-proof,” or “certified” can create rejection, recall, or warranty exposure. State the actual material, process, and test evidence. Applicability changes with destination market, intended use, chemical formulation, and whether the surface touches food, drinking water, or a regulated electrical assembly.
Iron plate selection is easier when procurement defines the cleaning endpoint
- Specify the substrate and finish. Call out grade, thickness, coating, roughness, and whether grinding or profile change is allowed.
- Describe the contaminant and next operation. A storage-rust instruction is different from a pre-paint or food-contact instruction.
- Set a controlled process. Name the cleaner, concentration, temperature, dwell time, rinse quality, drying method, and PPE.
- Define release evidence. Use photographs, a visual standard, pH or residue checks, and coating or weld-preparation tests where relevant.
- Plan packaging and storage. Add separators, desiccant, oil or approved temporary protection, and a maximum storage interval before reinspection.
For buyers sourcing conductive or fabricated components, DONGYAO can help align material documentation and configurable production for copper plate, copper busbar, and related assemblies. That support is most useful when the cleaning endpoint and downstream process are written before the order is released.
Frequently Asked Questions
What is an iron plate used for?
An iron or steel plate can serve as a structural, wear, tooling, electrical-support, or cooking surface. The required cleaning method depends on whether it will be welded, coated, energized, exposed to weather, or used for food. Confirm the drawing and service environment before selecting a chemical.
What are the different types of iron plates?
Common categories include low-carbon steel plate, higher-strength or alloy steel plate, cast iron plate, stainless steel plate, and coated or plated plate. “Iron plate” is often a trade description rather than a precise grade, so request the material standard and finish. Magnetic response alone is not enough for positive identification.
How can I safely clean an iron soleplate?
Unplug and cool the appliance, follow the maker’s instructions, and use a soft cloth or a product explicitly approved for the soleplate coating. Keep liquid away from electrical openings and do not scrape non-stick or plated surfaces with hard tools. Test a hidden edge first and wipe away all residue before use.
What is the standard Iron Plate recipe in Satisfactory?
In the game Satisfactory, the standard Iron Plate recipe uses three iron ingots to produce two iron plates in an equipment constructor. This game recipe has no connection to cleaning, cookware, or industrial material specifications; keep the terminology separate in purchasing documents.
References
- USDA FSIS: Cleaning and Sanitizing
- OSHA: Hazard Communication
- U.S. EPA: Clean Water Act summary
- ASTM International: Standards and test methods
- ISO 8501-1: Preparation of steel substrates before coating
Clean metal is not merely shiny metal: it is a surface whose chemistry, geometry, and intended use remain under control.
For a practical sourcing review, compare the required material and documentation in DONGYAO’s product categories, then contact the team with your grade, dimensions, cleaning endpoint, and destination market.
For related conductor products, view the product categories.